Tilt the table. Check every angle.
NC Proof Mill simulates 5-axis programs for the Haas UMC-750 (G254, G268, G253, G234 TCPC, G93) and Fanuc B / C tables (G68.2, G68.3, G68.4, G53.1, G53.6).
5-axis programs are the ones you least want to prove on the machine. NC Proof Mill turns the B tilt and C platter of a trunnion table the way the control does, cuts the stock with the part tilted, and checks the tool, the holder and the trunnion at every angle.
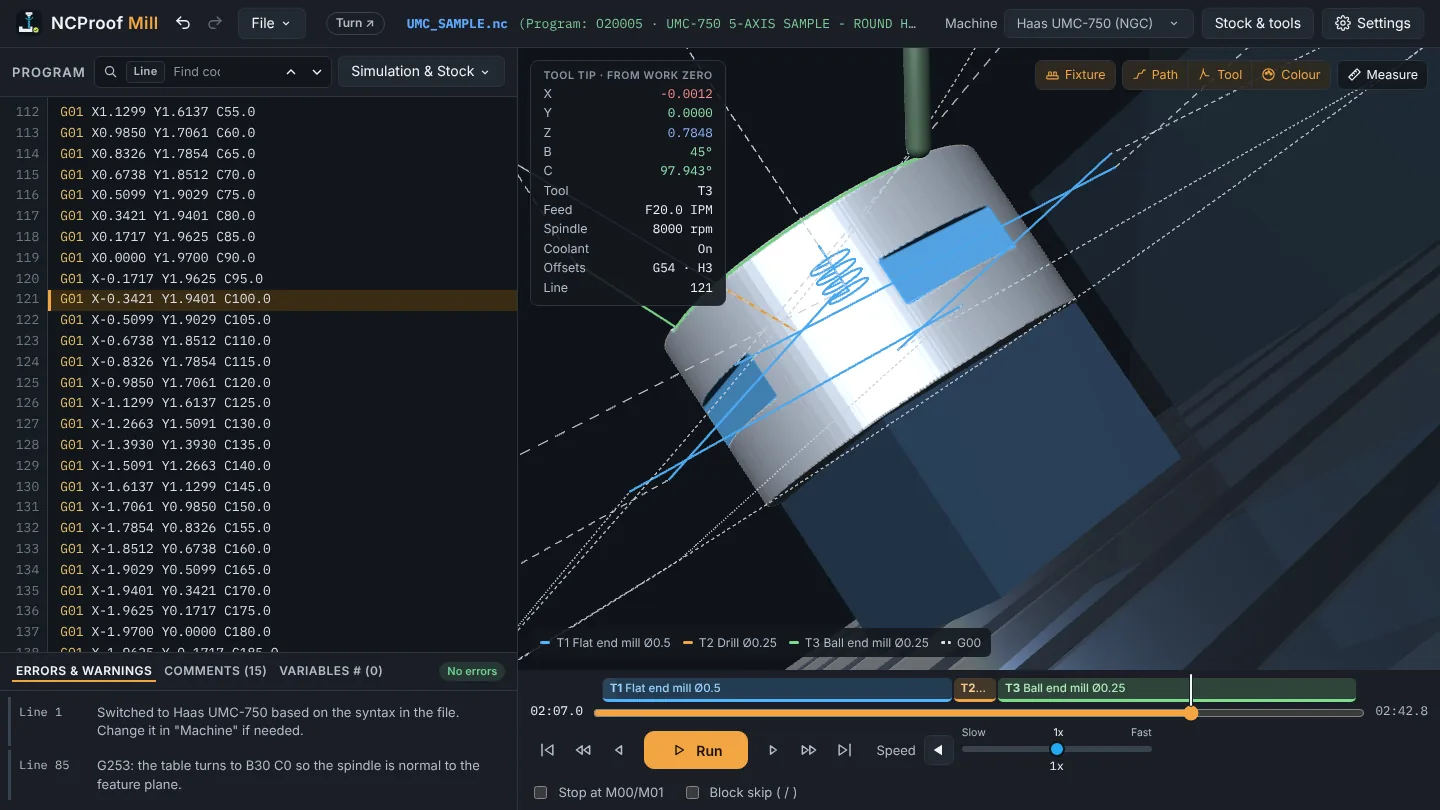
Haas UMC-750
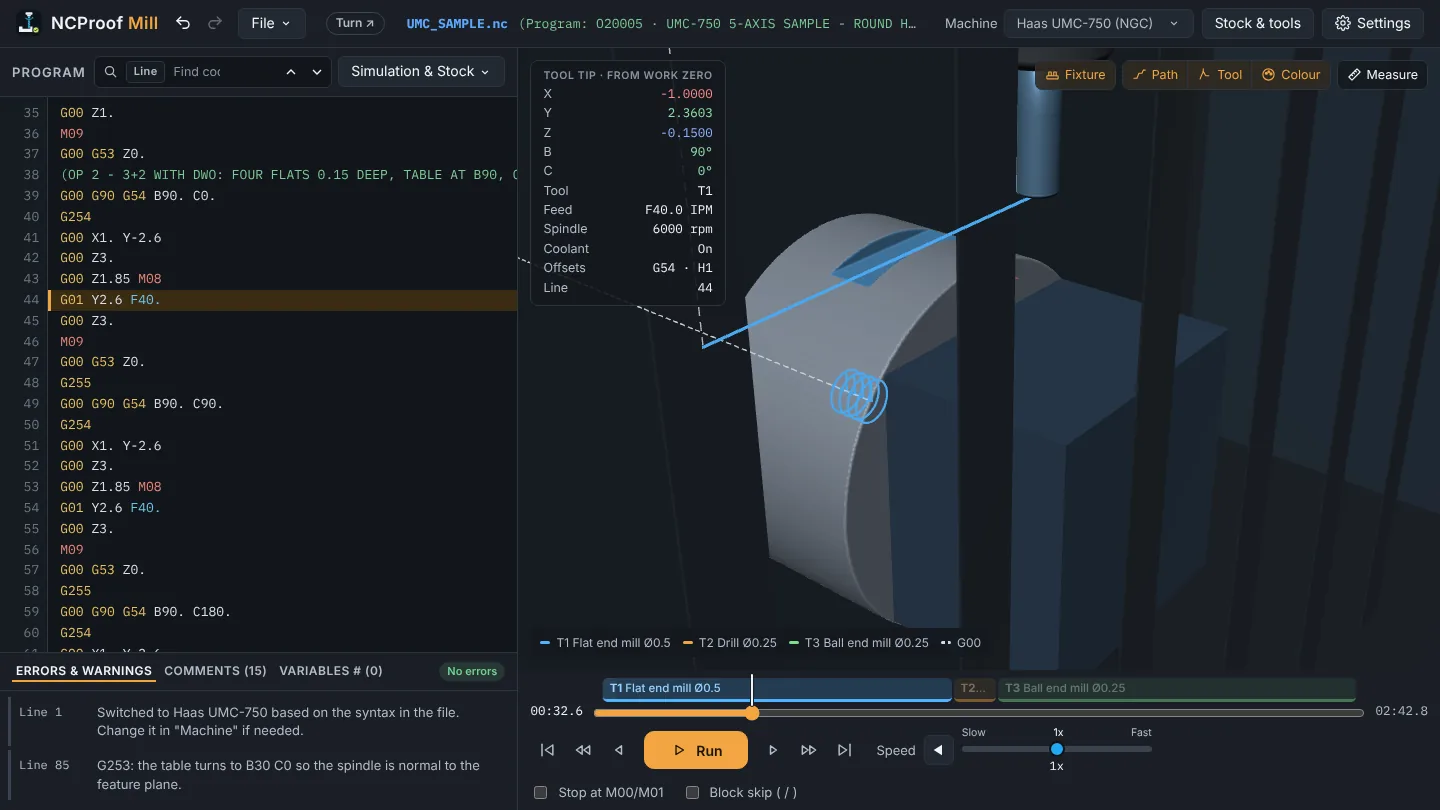
- 3+2 with DWO (G254 / G255): turn the table to a B / C angle and keep cutting in the part’s own X, Y and Z.
- Tilted planes (G268 / G269) and G253: define a feature plane and let the table turn so the spindle is normal to it. NC Proof tells you which B and C the table goes to.
- TCPC (G234): true simultaneous 5-axis moves, with the tool tip kept on the part while B and C turn, and G93 inverse-time feed.
- B / C work offsets, setups and round stock standing on the platter (set how high the part sits above it).
- Trunnion collisions: the tool and holder against the tilting trunnion and the platter, not only the part.
- B and C in the info panel as the table turns, in the angles of the program.
Fanuc 5-axis (B / C table)
For machining centres with a Fanuc control and a B / C trunnion table (sized like the UMC-750):
- G68.2 tilted working plane, with Euler angles and the P1–P4 forms, G68.3 (plane from the tool axis) and G68.4 (incremental).
- G53.1: the table turns to the angles of the tilted plane.
- G53.6: the table turns while the tool tip stays on the part.
How to use it
- Open a 5-axis program. NC Proof picks the Haas UMC-750 from the codes in the file, or choose it (or Fanuc · 5 axes B / C) in the Machine box.
- In Stock & tools → Fixture, check the stock on the platter and how high it sits.
- Press Ctrl+Enter to cut and check. Try the built-in sample O20005 · Haas UMC-750 to see 3+2, a tilted plane and TCPC in one program.
Step-by-step help: Guide, section 4: Stock, setups, machine and tools.